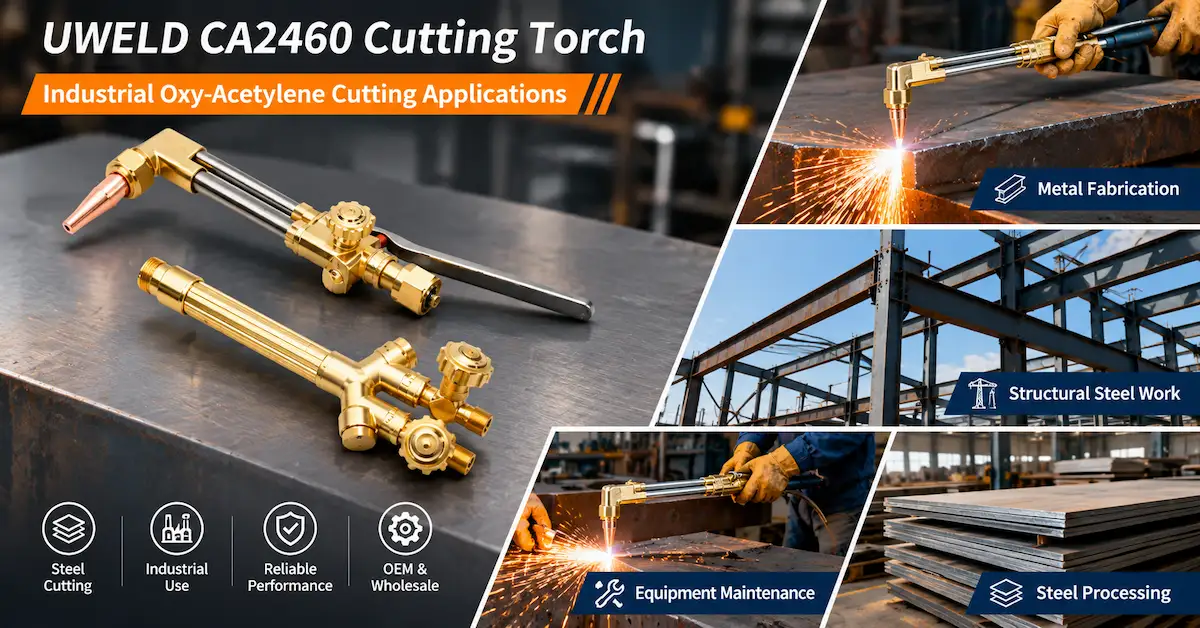
Quick Answer: The UWELD 1C005-0016 NM250 nozzle mix cutting torch is a heavy-duty hand cutting torch designed for suitable industrial steel cutting applications. It supports manufacturer-listed acetylene and propane configurations, with ANM/ANME nozzle families for acetylene and PNM/PNME families for propane. Buyers can evaluate 75°, 90°, and 180° head-angle options, different connection requirements, and the intended cutting-thickness range. Exact specifications should be established for the ordered configuration.
Industrial distributors and metal fabrication equipment importers face a common challenge when sourcing oxy-fuel cutting torches: a product may appear suitable for heavy-duty cutting while its nozzle family, fuel-gas arrangement, or torch dimensions differ from the customer's requirements.
The problem becomes more significant when buyers serve multiple markets with different gas supplies, cutting applications, and replacement-part requirements.
For example, supplying an acetylene nozzle to a customer operating an approved propane system can create a compatibility problem even when both nozzles are associated with the same torch family.
Likewise, purchasing a torch with an unsuitable head angle may make it more difficult for operators to access the intended workpiece.
UWELD, operated by Ningbo United Tools Co., Ltd., supplies professional gas cutting equipment and related accessories for international industrial customers.
This guide examines the NM250's nozzle-mix design, fuel-specific cutting tips, head-angle choices, industrial applications, and wholesale purchasing requirements.
Buyers can review the UWELD NM250 Heavy Duty Hand Cutting Torch when evaluating product configurations.
Key Takeaways: What Makes the NM250 Different?
-
Nozzle-mix construction: The NM250 uses a nozzle-mix arrangement designed for compatible oxy-fuel cutting operations.
-
Two fuel configurations: UWELD identifies both acetylene and propane as supported fuel options when the correct components are selected.
-
Fuel-specific cutting tips: ANM/ANME and PNM/PNME are separate nozzle families and should not be treated as interchangeable.
-
Multiple head angles: Published documentation lists 75°, 90°, and 180° options for different working-access requirements.
-
Heavy-duty construction: Product materials describe a forged brass head, stainless steel cutting lever, and backfire-resistant design.
-
Cutting capacity depends on configuration: Published 250 mm and 300 mm capacity references should be interpreted according to the exact nozzle and system.
-
Wholesale buyers need configuration control: Torch length, head angle, gas service, hose fitting, and replacement tips should be identified separately.
Technical selection principle: Choose the complete torch configuration around the intended fuel gas, nozzle family, steel thickness, and working position—not simply the highest advertised cutting capacity.
What Is the UWELD NM250 Heavy Duty Hand Cutting Torch?
The UWELD NM250 is a professional oxy-fuel hand cutting torch intended for suitable carbon steel and certain low-alloy steel applications.
It uses oxygen and an approved fuel gas to support thermal cutting through an oxidation reaction.
The torch's nozzle-mix construction and available cutting-head arrangements make it relevant to industrial fabrication, steel processing, structural work, and equipment maintenance.
NM250 Technical Specification Overview
| Specification | Published UWELD Information |
|---|---|
| Brand | UWELD |
| Model | NM250 |
| Product number | 1C005-0016 |
| Product type | Heavy-duty hand cutting torch |
| Mixing design | Nozzle-mix principle |
| Fuel configurations | Acetylene and propane |
| Acetylene nozzle families | YES, YES |
| Propane nozzle families | PNM, PNME |
| Head-angle options | 75°, 90°, 180° |
| Length reference in product title | 500 mm |
| Length reference in catalog illustration | 480 mm |
| Cutting capacity in product overview | Up to 300 mm mild steel |
| Cutting capacity in illustrated materials | Up to 250 mm |
| Hose connection reference | BSP 3/8", with other options described |
| Head construction | Die-forged brass, as described in product materials |
| Lever | Stainless steel lever with hold-down feature |
| Applications | Industrial steel cutting and maintenance |
| Purchasing options | Wholesale and OEM/ODM inquiries |
Source: UWELD 1C005-0016 product listing and associated catalog illustration. Length and capacity references describe the published source materials and should not be combined into a single unverified specification.
Why Is the NM250 Considered Heavy Duty?
The NM250 is positioned for industrial cutting applications involving substantial steel sections and demanding workshop environments.
Its published design features include a forged brass cutting head, metal gas tubes, and a stainless steel cutting lever.
These construction details are relevant to durability and handling.
However, a heavy-duty designation does not independently establish the torch's service life, allowable duty cycle, or cutting performance with every nozzle.
Those characteristics depend on the approved assembly and working conditions.
How Does Nozzle-Mix Technology Work?
The NM250 nozzle mix cutting torch uses a mixing arrangement associated with the cutting nozzle.
In oxy-fuel cutting, a fuel-gas and oxygen flame first heats the workpiece to the temperature required for rapid oxidation.
A separate concentrated cutting oxygen stream then reacts with the heated steel, producing oxides that are removed from the cutting path.
The cutting nozzle plays an important role in both preheating and cutting oxygen delivery.
Nozzle-Mix vs Other Torch Mixing Arrangements
| Evaluation | Nozzle-Mix Torch | Other Approved Mixing Designs |
|---|---|---|
| Gas mixing | Associated with the nozzle-end arrangement | Depends on torch design |
| Nozzle selection | Must match the specified fuel and torch | Must match the approved design |
| Cutting performance | Depends on nozzle, oxygen supply, fuel and material | Also depends on system configuration |
| Safety | Requires approved protection and operating procedures | Requires approved protection and procedures |
| Replacement parts | Fuel-specific nozzle family is important | Design-specific consumables are important |
A nozzle-mix design should not be described as eliminating the possibility of backfire or flashback.
UWELD's material describes the NM250 as having a backfire-resistant design, but safe operation still requires correctly selected equipment, qualified personnel, and appropriate protective devices.
What Is the Role of the Cutting Oxygen Valve?
The product material describes a cutting oxygen flow valve intended to support progressive piercing and smooth cutting control.
This refers to the designed operating characteristics of the torch.
However, actual cutting performance depends on the complete system.
Purchasing managers should assess the valve's functionality and assembly quality through appropriate sample inspection rather than assume a specific measured performance improvement.
ANM vs PNM: Which Cutting Nozzle Is Right for the NM250?
Fuel-specific nozzle selection is one of the most important aspects of purchasing this torch.
UWELD identifies four relevant nozzle families:
-
ANM and ANME for acetylene configurations.
-
PNM and PNME for propane configurations.
The correct nozzle must also match the selected torch head, seating design, and required steel thickness.
NM250 Fuel and Cutting Nozzle Compatibility
| Nozzle Family | Intended Fuel Configuration | Main Buyer Requirement |
|---|---|---|
| ANM | Acetylene | Verify approved torch fit, size and cutting range |
| LOVE | Acetylene | Verify specific nozzle variant and seat |
| PNM | Propane | Confirm propane-compatible configuration |
| PNME | Propane | Confirm exact nozzle type and associated components |
These are manufacturer-listed families, not a statement that all individual sizes are interchangeable.
Why Must Acetylene and Propane Nozzles Be Distinguished?
Acetylene and propane have different combustion characteristics.
Their approved cutting nozzles may use different preheating passage arrangements and component construction.
A distributor should not substitute a propane nozzle for an acetylene nozzle based on similar size markings or appearance.
The correct configuration also requires suitable regulators, hoses, oxygen delivery, and protective equipment.
Relevant UWELD Replacement Nozzle Products
UWELD's product range includes:
1C001-0040 — ANM/ANME Acetylene Cutting Nozzles
These are listed as one-piece tellurium copper cutting nozzle configurations for compatible acetylene applications.
1C001-0041 — PNM/PNME Propane/Natural Gas Cutting Nozzles
These are listed as two-piece cutting nozzle configurations for the specified fuel services.
The presence of these nozzle families in the UWELD catalog supports replacement-part sourcing, but purchasers must verify the exact model, nozzle size, seating design, and approved pairing with their NM250 configuration.
For broader product-selection guidance, read the UWELD Cutting Torch Nozzle Selection Guide.
How Do 75°, 90° and 180° Head Angles Affect Torch Selection?
Head angle affects the working geometry of a hand cutting torch.
Different positions and workpiece arrangements may require different access and handling characteristics.
UWELD's NM250 documentation lists 75°, 90° and 180° head-angle options.
These should be understood as available configuration choices, not three heads included with every torch.
Head-Angle Selection Matrix
| Head Angle | Potential Selection Consideration | What Buyers Should Evaluate |
|---|---|---|
| 75° | Alternative approach to angled or restricted work | Workpiece geometry and operator access |
| 90° | Conventional perpendicular head arrangement | General fabrication and cutting position |
| 180° | Straight-line or alternative access requirements | Torch orientation, clearance and handling |
When Is a 90° Cutting Head Appropriate?
A 90° head arrangement may suit general manual cutting situations where the operator needs an approximately perpendicular working orientation relative to the torch body.
However, torch positioning should follow the approved cutting procedure and equipment design.
When Should Buyers Consider 75° or 180°?
Alternative head angles may be relevant when workpiece access, surrounding structures, or handling preferences differ from conventional applications.
For example, structural steel assemblies or maintenance environments may restrict the approach to a cutting location.
The most suitable angle should be evaluated using the actual workpiece geometry and intended operating conditions.
Why Head-Angle Selection Matters for Distributors
A distributor stocking the NM250 for multiple customer groups should identify which head configurations its customers actually require.
Providing one angle as a universal solution may not satisfy every industrial application.
A better approach is to document demand by head angle and maintain clear identification for each approved configuration.
How Long Is the UWELD NM250 Cutting Torch?
The product title describes a 500 mm cutting torch, while the provided catalog illustration identifies a length of 480 mm.
These figures are close but should not be automatically treated as identical.
Torch Length Comparison
| Published Reference | Length | What It Establishes |
|---|---|---|
| UWELD product title | 500 mm | Product's nominal commercial description |
| UWELD catalog illustration | 480 mm | A listed dimensional reference |
| Other available configurations | Not established for 1C005-0016 | Requires individual product identification |
A nominal commercial length and a technical drawing dimension may be measured differently.
However, without a defined measurement method or approved drawing, the difference should not be explained as a confirmed tolerance.
Why Torch Length Matters
Torch length influences working reach, handling, transport, and access around steel structures.
For a fabrication workshop, a standard hand torch may be sufficient.
For maintenance work involving restricted access or large equipment, working reach can become more important.
What Should Wholesale Buyers Record?
An RFQ should identify the required overall length, measurement reference, head angle, and intended application.
For repeat purchases, the approved dimension should be included in the controlled product specification.
Can the NM250 Cut 250 mm or 300 mm Steel?
The NM250 is marketed for substantial steel-cutting applications.
However, its published materials show different maximum cutting-capacity references.
The product overview states up to 300 mm mild steel, while the supplied technical illustration describes cutting up to 250 mm.
Understanding the Capacity References
| Published Claim | How It Should Be Interpreted |
|---|---|
| Up to 250 mm | Capacity claim shown in the product illustration |
| Up to 300 mm | Capacity claim appearing in the current product overview |
| Actual cutting capability | Depends on the approved nozzle and complete gas system |
These values should not be treated as proof that every NM250 configuration can cut the stated thickness.
What Determines Maximum Cutting Thickness?
The ability to cut thick steel depends on several factors:
-
The approved cutting nozzle and its size.
-
Cutting oxygen delivery capacity.
-
Fuel-gas configuration.
-
Steel grade and material condition.
-
Torch and nozzle design.
-
Applicable manufacturer operating procedures.
For example, a nozzle selected for routine fabrication work may not provide the required capacity for the maximum thickness advertised for the wider torch family.
How Should Industrial Buyers Use These Figures?
The safest purchasing approach is to specify the normal cutting-thickness range and the maximum required thickness.
The supplier can then identify the appropriate torch and nozzle arrangement.
A distributor should avoid using the largest published capacity as a universal performance promise without a supporting model-specific specification.
Purchasing principle: Match cutting capability to the complete approved setup, not the torch body alone.
Where Is the NM250 Hand Cutting Torch Used?
The NM250 nozzle mix cutting torch is relevant to industrial applications involving suitable carbon steel cutting.
Potential buyers include fabrication shops, structural steel contractors, industrial maintenance businesses, equipment distributors, and professional tool suppliers.
Industrial Application Matrix
| Application | Typical Requirement | Key Product Consideration |
|---|---|---|
| Heavy steel fabrication | Cutting thicker carbon steel sections | Approved nozzle and capacity |
| Structural steel work | Cutting steel beams and components | Head angle and reach |
| Industrial maintenance | Repair and component removal | Equipment access and serviceability |
| Construction | Suitable on-site steel cutting | Handling and system safety |
| Steel processing | Repeated plate and section cutting | Nozzle replacement and consistency |
| Equipment distribution | Supplying professional cutting systems | SKU identification and consumable availability |
Heavy Steel Fabrication
Fabrication workshops may use oxy-fuel equipment to cut carbon steel plates and structural components.
For demanding applications, the torch, nozzle, oxygen supply, and cutting conditions must be selected together.
Construction and Structural Work
Construction environments may introduce restricted working positions and site-specific safety requirements.
The NM250's available head-angle configurations are worth evaluating for different workpiece arrangements.
Industrial Maintenance
Maintenance teams may use oxy-fuel cutting equipment to remove damaged steel components and perform approved repair operations.
Torch access, correct gas connections, replacement parts, and suitable protective equipment are important considerations.
Who Should Consider a Different Cutting Technology?
Conventional oxy-fuel cutting is generally not the preferred choice for stainless steel or aluminum.
Applications requiring narrow kerfs, intricate profiles, or high-speed thin-sheet cutting may be better served by suitable plasma, laser, or mechanical equipment.
An industrial purchasing guide should explain these limitations rather than position one torch as suitable for every metal.
How Does the NM250 Compare With Other UWELD Cutting Torches?
UWELD offers multiple cutting torch configurations serving different industrial applications.
The NM250 is especially relevant to buyers evaluating nozzle-mix technology and fuel-specific replacement nozzles.
UWELD Cutting Torch Comparison
| Product | Published Positioning | Primary Selection Focus |
|---|---|---|
| NM250 / 1C005-0016 | Heavy-duty nozzle-mix hand cutting torch | Fuel-specific nozzles, head angle, cutting configuration |
| CA2460 / 1C005-0002 | Heavy-duty cutting attachment with 1-1-101 tip | Compatible handle and cutting attachment |
| 1C005-0003 | Heavy-duty cutting torch with check-valve features | Complete torch configuration and accessories |
| 1C005-0012 | Straight cutting torch with triangular stainless steel tubes | Straight-style torch construction and applications |
The table compares product configurations rather than claiming that one model has greater durability or cutting performance.
When Is the NM250 a Better Candidate?
The NM250 is worth evaluating when buyers specifically require its listed nozzle-mix configuration, ANM/ANME or PNM/PNME nozzle families, and available head-angle arrangements.
When Should Buyers Consider the CA2460?
The CA2460 may be a relevant alternative when the customer requires its particular cutting attachment, handle compatibility, or cutting-tip family.
The two product families should not be treated as direct substitutes without technical verification.
What Quality-Control Checks Matter for the NM250?
A professional cutting torch should be evaluated through its approved components, assembly quality, and suitable functional verification.
A product photograph does not establish manufacturing consistency.
Recommended NM250 Quality Inspection Checklist
| Inspection Area | What Buyers Should Verify |
|---|---|
| Model identification | Correct NM250 / 1C005-0016 |
| Head angle | Approved 75°, 90° or 180° configuration |
| Torch length | Agreed dimension and measurement method |
| Fuel-gas configuration | Correct acetylene or propane version |
| Cutting nozzle | Approved ANM/ANME or PNM/PNME family and size |
| Brass head | Material specification and construction |
| Gas tubes | Correct assembly and physical condition |
| Cutting oxygen lever | Required mechanical function |
| Flow-control valves | Correct assembly and operation |
| Hose connections | Approved thread and fitting arrangement |
| Gas-tightness | Applicable leakage-test records |
| Safety-related components | Correct design and documented functions |
| Packaging | Product identification and accessory completeness |
| Traceability | Order and approved specification reference |
Why Are Nozzle Seating and Gas Passages Important?
The nozzle and torch head must have compatible mating geometry.
Gas passages should conform to the approved design.
Incorrect assembly or dimensions can create equipment compatibility problems or unsuitable gas-flow conditions.
For wholesalers, dimensional inspection and clear replacement-part references support more consistent customer service.
How Should Functional Testing Be Handled?
Functional testing should reflect the approved equipment configuration.
Relevant checks may include assembly integrity, gas-tightness verification, valve operation, and other product-specific requirements.
Gas-system testing must be performed by qualified personnel using approved procedures.
A manufacturer should provide the inspection documents applicable to the actual supplied model.
What Safety and Standards Requirements Apply?
Oxy-fuel cutting involves pressurized oxygen, flammable gases, high temperatures, and potential backfire or flashback hazards.
Qualified operators must use equipment approved for the intended gas system and follow the applicable instructions.
Nozzle-Mix Design Is Not a Substitute for Protection
UWELD's product materials describe the NM250 as having a backfire-resistant design.
However, this should not be interpreted as guaranteed protection against every hazardous gas-system condition.
Appropriate protective devices, gas-specific regulators, hoses, and correct operating procedures remain essential.
Check Valves and Flashback Arrestors
A check valve is designed to restrict reverse flow under specified conditions.
A flashback arrestor is designed to prevent flame propagation under its rated conditions.
These functions are not automatically equivalent.
The required devices should be established for the complete gas system.
BS EN ISO 5172 and Product Compliance
UWELD's product description references BS EN ISO 5172 compliance.
ISO 5172:2006, including its applicable amendments, specifies requirements and tests for gas welding, heating, and cutting blowpipes.
Its published scope includes relevant cutting blowpipes with a cutting range up to 300 mm.
However, the scope of a standard is not evidence that every covered product can cut 300 mm steel.
Likewise, a product-page compliance statement does not establish independent certification for every available NM250 configuration.
Industrial buyers should request the current model-specific conformity or testing documents required for their destination market.
How Should Distributors Evaluate NM250 Wholesale Costs?
Purchasing costs depend on more than the listed torch price.
Different head angles, fuel configurations, cutting nozzles, connection options, and packaging requirements may affect the commercial quotation.
Total Sourcing Cost
Total Sourcing Cost = Torch Purchase Cost + Compatible Nozzles + Inspection + Packaging + Freight + Inventory + Expected After-Sales Costs
| Cost Factor | Purchasing Consideration |
|---|---|
| Torch configuration | Selected head angle and assembly |
| Fuel-gas version | Acetylene or propane components |
| Cutting nozzles | Approved sizes and replacement quantities |
| Hose connections | Standard or market-specific configuration |
| Sample approval | Technical and inspection requirements |
| OEM branding | Labels, packaging and artwork |
| Wholesale quantity | MOQ and order conditions |
| Spare parts | Long-term replacement availability |
| Shipping | Shipment size and destination |
| After-sales | Product identification and service support |
Why Is Replacement Nozzle Availability Important?
Cutting nozzles are replaceable working components.
For industrial users, having the correct replacement nozzle available helps avoid unnecessary maintenance delays.
For distributors, the ability to reorder compatible nozzles can support repeat sales and customer service.
However, stocking too many similar nozzle configurations may increase inventory complexity.
A balanced purchasing program should match nozzle inventory to the installed torch base and actual customer demand.
Is the Lowest Torch Price Always the Best Value?
Not necessarily.
A lower price can offer good value when the configuration is suitable and quality requirements are met.
However, incorrect fuel-gas components, wrong nozzle sizes, or unsuitable hose fittings can create additional purchasing and service costs.
The most meaningful comparison uses technically equivalent product configurations.
How Can Buyers Choose the Right NM250 in Three Steps?
Step 1: Define the Cutting Application
Identify the material, typical steel thickness, required access, working environment, and expected cutting frequency.
Determine whether the customer needs a particular head angle or torch length.
Decision: Select an application-appropriate configuration rather than relying on the maximum advertised cutting capacity.
Step 2: Match Fuel Gas, Nozzle and Connections
Confirm whether the equipment will use an approved acetylene or propane system.
Select the appropriate nozzle family and verify the intended hose fittings and protective accessories.
Decision: Approve only the complete compatible equipment arrangement.
Step 3: Verify Quality and Commercial Requirements
Review the approved specification, product samples, inspection records, packaging, MOQ, lead time, and spare-parts arrangements.
Decision: Choose the configuration that offers a suitable combination of technical fit, documented quality, and purchasing value.
For product-specific assistance, visit the UWELD NM250 product page.
Practical Sourcing Scenario: One NM250 Product Family for Two Fuel-Gas Markets
Consider an industrial equipment distributor serving two groups of professional customers.
The first group operates oxygen-acetylene equipment.
The second group uses approved oxygen-propane systems.
Both are interested in the NM250 hand cutting torch.
This is an illustrative purchasing scenario rather than a documented UWELD customer project.
The Purchasing Challenge
The distributor initially wants to supply one universal torch and nozzle combination.
However, the published NM250 specifications identify different nozzle families for acetylene and propane applications.
Customers also have different requirements concerning cutting-head angle and working access.
Recommended Procurement Approach
1. Separate the fuel configurations. Identify the required acetylene and propane versions.
2. Establish nozzle compatibility. Record the approved ANM/ANME or PNM/PNME nozzles and required sizes.
3. Define head-angle requirements. Confirm the 75°, 90°, or 180° options required by each market.
4. Approve the product specification. Identify torch length, hose connections, accessories and product labeling.
5. Establish repeat-order controls. Maintain distinct SKU references and approved product documents.
Expected Commercial Benefits
This approach can reduce product-selection confusion, improve replacement-part identification, and make future purchasing more manageable.
Any numerical improvements in return rates, inventory costs, or customer satisfaction would need to be established using actual distributor records.
The main lesson is that fuel-specific configuration and nozzle identification should be established before wholesale inventory is expanded.
OEM/ODM and Wholesale NM250 Cutting Torch Supply
UWELD supports international wholesale and OEM/ODM inquiries for welding and cutting equipment.
Depending on technical feasibility, projects may involve branding, product identification, packaging, selected accessories, and approved configuration adjustments.
Recommended OEM Purchasing Workflow
| Stage | Main Requirement |
|---|---|
| Requirements review | Define application, fuel and target market |
| Product selection | Choose the NM250 configuration |
| Technical confirmation | Identify nozzles, head angle, length and connections |
| Sample approval | Review component quality and compatibility |
| Branding | Approve product labels and packaging |
| Production | Establish the approved specification |
| Quality inspection | Verify agreed acceptance criteria |
| Shipment | Confirm quantities and documentation |
| Repeat orders | Maintain approved component references |
Changes affecting gas passages, connections, mixing design, or safety-related components require appropriate technical review.
MOQ and Delivery Considerations
UWELD's FAQ page explains that minimum order quantities depend on product and customization requirements.
Product availability, sample arrangements, and delivery schedules should be confirmed individually.
For NM250 orders involving different head angles or fuel configurations, buyers should request separate quantities and availability information for each approved variant.
What Should Be Included in an NM250 Wholesale RFQ?
A detailed request for quotation helps the supplier identify the correct torch configuration.
Recommended RFQ Checklist
| RFQ Field | Information Required |
|---|---|
| Product | NM250 nozzle-mix hand cutting torch |
| Model | UWELD 1C005-0016 |
| Application | Steel fabrication, structural work, maintenance |
| Fuel gas | Acetylene or propane |
| Cutting nozzle | ANM, ANME, PNM or PNME |
| Nozzle size | Required size and quantity |
| Steel thickness | Typical and maximum application range |
| Head angle | 75°, 90° or 180° |
| Torch length | Required measurement and configuration |
| Hose connection | Required thread and gas-service arrangement |
| Protective equipment | Required approved devices |
| Quality documents | Technical specification and inspection records |
| Product branding | UWELD or private-label |
| Packaging | Standard or customized |
| Purchase volume | Samples, initial order and projected repeat demand |
| Destination market | Country or region |
| Commercial terms | Requested schedule and delivery requirements |
A complete RFQ should distinguish the intended fuel-gas configuration and replacement nozzles before the commercial quotation is finalized.
Looking for an NM250 nozzle mix cutting torch for industrial distribution? Contact UWELD to request current product specifications, compatible nozzle information, head-angle options, OEM packaging details and wholesale pricing.
Frequently Asked Questions About the NM250 Nozzle-Mix Cutting Torch
1. What is the UWELD NM250 cutting torch?
The UWELD NM250, model 1C005-0016, is a heavy-duty hand cutting torch with a nozzle-mix design. It is intended for suitable industrial oxy-fuel steel cutting applications.
2. Can the NM250 use both acetylene and propane?
UWELD lists approved configurations for acetylene and propane. The complete equipment system must use the correct fuel-specific nozzles, regulators, hoses, and protective devices.
3. Which nozzles are used with the NM250?
The published NM250 documentation lists ANM and ANME for acetylene configurations, and PNM and PNME for propane configurations. Buyers should confirm exact nozzle sizes and compatibility for the selected torch.
4. What head angles are available?
UWELD lists 75°, 90° and 180° head-angle options. The required version should be specified when ordering; these angles are not necessarily included with one product.
5. Is the NM250 480 mm or 500 mm long?
The product title describes 500 mm, while the catalog illustration identifies 480 mm. Buyers should specify the required length and obtain the approved dimensional reference for their order.
6. Can the NM250 cut 300 mm steel?
The product overview advertises cutting up to 300 mm mild steel, while another illustration lists up to 250 mm. The capability of a particular torch and nozzle combination should be established using the approved technical specification.
7. What is the advantage of a nozzle-mix cutting torch?
A nozzle-mix design places the mixing arrangement near the working end of the torch. Its suitability depends on the approved construction and complete gas system. It does not eliminate the need for flashback protection and correct operating procedures.
8. What hose connection does the NM250 use?
The product illustration references BSP 3/8" connections and mentions other available thread options. Buyers should confirm the exact thread, fitting arrangement, and gas compatibility for the required version.
9. What should distributors inspect before bulk purchasing?
Important checks include the model, fuel configuration, nozzle family, head angle, length, connections, material specifications, valve function, gas integrity, packaging and product identification.
10. Does UWELD support OEM and wholesale NM250 orders?
UWELD supports wholesale and OEM/ODM inquiries for cutting equipment. Available customization, nozzle combinations, order quantities and lead times should be confirmed for the individual project.
Conclusion
Selecting an NM250 nozzle mix cutting torch requires more than comparing a product photograph, nominal length, or maximum cutting-thickness claim.
The UWELD 1C005-0016 offers a heavy-duty hand cutting torch platform with manufacturer-listed acetylene and propane configurations, ANM/ANME and PNM/PNME nozzle families, and different head-angle options.
For industrial distributors and equipment importers, the most important purchasing considerations are fuel compatibility, cutting nozzle selection, torch dimensions, working access, hose fittings, and reliable replacement-part identification.
The published 480 mm/500 mm length references and 250 mm/300 mm cutting-capacity descriptions should be treated as configuration details rather than combined into unverified performance claims.
For OEM brands, consistent product identification, approved samples, suitable quality documentation and controlled repeat orders also contribute to long-term purchasing reliability.
UWELD supplies professional gas cutting tools, regulators, cutting nozzles and related industrial equipment for international customers.
To evaluate an appropriate configuration, visit the UWELD NM250 Heavy Duty Hand Cutting Torch, explore UWELD Gas Cutting Products, or contact UWELD for nozzle compatibility details, technical specifications, samples, OEM options and a wholesale quotation.